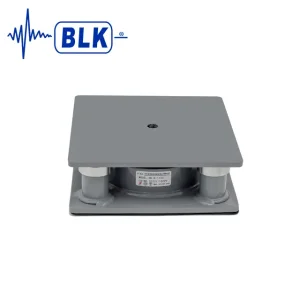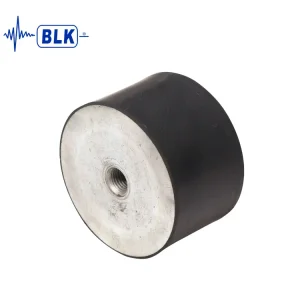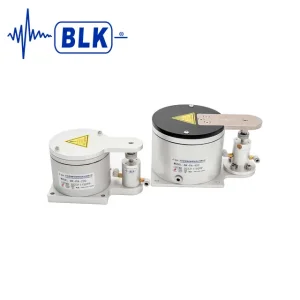
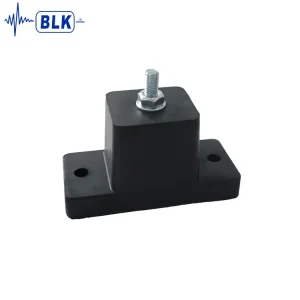
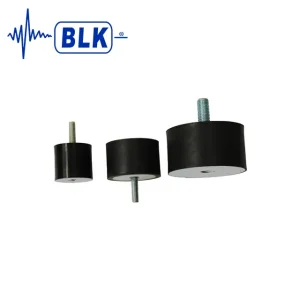
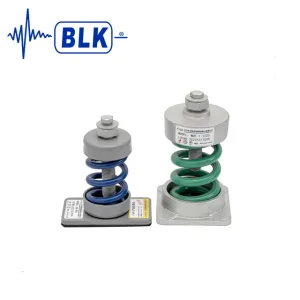
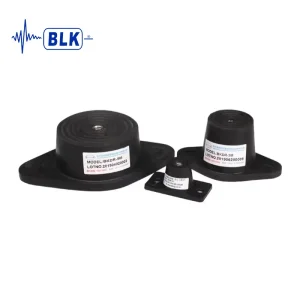
Featured Air Compressor Vibration Isolation Products
Explore our primary industrial isolation solutions engineered specifically to damp high-frequency harmonics, structural resonance, and operational fatigue in rotary screw and reciprocating compressors.
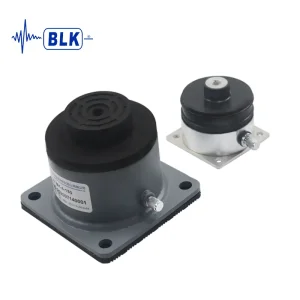
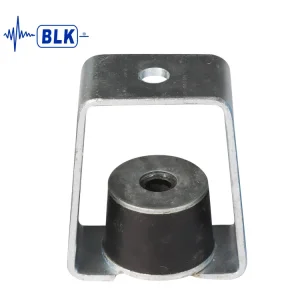
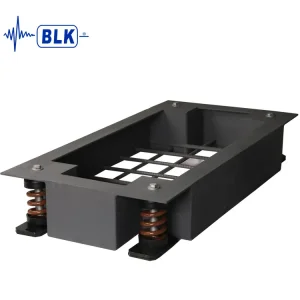
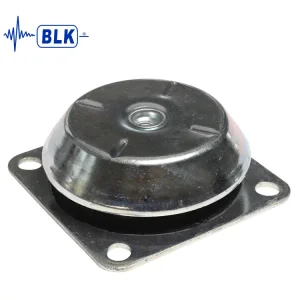
1. Engineering Fundamentals of Air Compressor Vibration Mitigation
Air compressors—whether rotary screw, centrifugal, or reciprocating piston configurations—generate severe dynamic forces during operation. These forces manifest as both high-frequency structural vibration and low-frequency cyclical shock loads. Unmitigated vibrational kinetic energy transfers directly into building foundations, structural steel frameworks, and adjacent piping networks. Over time, this uncontrolled energy transfer causes premature mechanical wear, structural fatigue, pipe weld failures, air line joint leaks, and unacceptably high ambient noise levels in industrial facilities.
As a specialized Custom Air Compressor Anti Vibration Mounts Factory & Manufacturer, our engineering philosophy is grounded in precise dynamic isolation theory. Effective vibration isolation requires matching the stiffness ($K$) and damping coefficient ($C$) of the elastomeric or spring isolator to the specific operating disturbance frequency ($f_d$) of the compressor block.
Rotary Screw Dynamics
Rotary screw compressors produce dominant high-frequency harmonic vibrations resulting from male and female meshing rotors (ranging from 500 Hz to 3,000 Hz). These require high-damping polymer matrix pads or bonded rubber-to-metal mounts engineered to absorb acoustic waves and high-frequency structural hum.
Reciprocating Piston Shock
Reciprocating compressors exhibit heavy low-frequency unbalanced inertial forces (10 Hz to 60 Hz) driven by crank-piston movement. Isolating these forces mandates heavy-duty open spring mounts or multi-directional rubber isolators designed with high deflection capacity to prevent structural resonance.
Inverter-Driven (VFD) Units
Variable Frequency Drive (VFD) air compressors sweep across wide RPM bands during modulation. Anti-vibration mounts must be mathematically modeled to ensure the system natural frequency ($f_n$) never coincides with the variable operational frequencies, completely eliminating harmonic lock-in.
Mathematical Foundation of Isolation Efficiency ($E$)
The mathematical transmissibility ($T$) of an isolator is expressed by the equation:
Where $r = f_d / f_n$ (ratio of forcing frequency to natural frequency) and $\zeta$ is the damping ratio. To achieve greater than 92% isolation efficiency ($E = 1 - T$), the frequency ratio $r$ must be maintained above $\sqrt{2}$, with an optimal targeting zone of $r \ge 3.0$.
Proven Global Manufacturing Competence
Our manufacturing center combines material science expertise with robotic automation to deliver field-tested anti-vibration products to top-tier global OEM air compressor brands.
2. Global Procurement Criteria & Total Cost of Ownership (TCO)
For global procurement directors, industrial plant engineers, and original equipment manufacturers (OEMs), choosing the correct anti-vibration mounting solution is a critical decision impacting lifecycle operational expenditure (OPEX). Low-grade commercial off-the-shelf rubber isolators suffer from rapid compression set, chemical hardening due to ambient oil mist, and ozone degradation, leading to total loss of dampening properties within 12 to 18 months.
| Evaluation Parameter | Standard Commercial Mounts | Bellking Custom OEM Compressor Mounts | Impact on Plant Operations |
|---|---|---|---|
| Elastomeric Material | Recycled Nitrile / Lower Grade NR | Virgin High-Grade NBR, EPDM, Silicone, or Neoprene | Resistance to lubricating oil mist, heat up to 120°C, and ozone aging. |
| Dynamic Stiffness Ratio ($K_d/K_s$) | High (> 2.2) - High Dynamic Stiffening | Controlled Low Ratio (1.35 to 1.6) | Prevents energy transmission under dynamic load while maintaining static alignment. |
| Metal-to-Rubber Bonding | Single-stage basic adhesive bond | Dual-layer chemical silane vulcanization bonding | Zero risk of shear detachment under 3G-5G severe dynamic start-up shock loads. |
| Corrosion Protection | Standard Electro-galvanizing (<96h) | Dacromet / Epoxy Coating (900h Salt Spray) | Eliminates structural rust in harsh offshore, coastal, or high-humidity environments. |
| Lifecycle Expectancy | 1 - 2 Years | 10 - 15+ Years (Spring) / 8+ Years (Rubber) | Reduces replacement downtime and protects expensive air compressor air-ends. |
Investing in specialized custom anti-vibration mounts lowers the Total Cost of Ownership (TCO) by protecting high-value capital equipment. Unmitigated vibration accelerates bearing fatigue inside the compressor screw block, misaligns direct-drive couplings, causes structural fractures in heat exchangers, and damages electronic VFD control panels. Implementing precision-engineered mounts extends overall compressor overhaul intervals by up to 40%.
3. Strategic Supply Chain Advantages of Our Chinese Manufacturing Hub
Operating directly out of Kunshan, Jiangsu—one of China's primary advanced manufacturing corridors—our production facility offers global clients an optimal balance of engineering precision, industrial scalability, and cost competitiveness.
Complete Upstream Integration
Our localized supply network provides rapid access to specialized raw materials including high-tensile spring alloy steel (60Si2Mn), custom-formulated synthetic elastomeric compounds, and precision CNC-machined metal hardware. This localized integration reduces raw material lead times to days rather than weeks.
Advanced Tooling & Injection
Equipped with automated rubber injection molding presses, robotic welding cells, and dynamic fatigue testing machinery, our factory produces over 100,000 unit assemblies per year with strict dimensional repeatability (tolerances within ±0.05mm).
Agile Rapid Prototyping
Unlike traditional Western suppliers constrained by high tooling costs and long schedule queues, our engineering design team provides custom prototype samples in as few as 3 to 5 working days following 3D CAD step file approval and Finite Element Analysis (FEA) verification.
Direct Factory Pricing
By eliminating intermediary trading company markups and streamlining manufacturing overheads, we pass direct 20% to 35% cost savings to global OEMs without compromising on international engineering standards or material quality.
4. Field Application Scenarios & Engineering Deployments
Air compressor installations vary wildly across different operational environments. A mount designed for an indoor cleanroom compressed air station will fail if placed on an offshore oil rig or a mobile diesel road-construction compressor. Below are key field scenarios where custom isolation engineering is vital:
Cleanroom & Medical Oil-Free Air Stations
Pharmaceutical and semiconductor fabrication plants require ultra-pure, oil-free compressed air. In these facilities, micro-vibrations transmitted into raised cleanroom flooring ruin sensitive metrology equipment. We supply high-damping, non-outgassing silicone and specialized EPDM mounts that meet cleanroom Class 10/ISO Class 4 standards.
Heavy Industrial Plant Utility Rooms
Large manufacturing plants feature centralized air compressor banks containing multiple 250kW+ rotary screw compressors mounted adjacent to chillers and water pumps. Installing heavy inertia base frame systems combined with BK-Type spring mounts decouples the high-tonnage dynamic shock loads from the factory floor slab.
Mobile Diesel Air Compressors & Mining Rig Systems
Portable compressors towed behind vehicles or mounted on drilling rigs face extreme multi-axial dynamic vector loads, transient shocks during transport, and aggressive weather exposure. Our captive, shear-protected custom rubber mounts lock the engine-compressor skid safely even in rollover or heavy incline conditions.
5. Regulatory Compliance & Localized Technical Support
Global equipment manufacturers cannot afford compliance bottlenecks or import rejections. All custom mounts produced at our factory comply with major international environmental and mechanical safety directives:
REACH & RoHS Compliance
Every rubber formulation is thoroughly tested to guarantee zero SVHCs (Substances of Very High Concern), polycyclic aromatic hydrocarbons (PAHs), heavy metals, or toxic plasticizers. Certificates of compliance accompany every export shipment.
ISO 9001 Quality Oversight
From raw polymer batch inspection using rheometers to 100% dynamic load testing of finished spring assemblies, our ISO 9001 quality system guarantees zero-defect manufacturing and full lot traceability.
Localized Technical Engineering
We provide 24/7 localized engineering assistance for international clients. Our technical sales team delivers tailored vibration calculation reports, 3D CAD step files, installation diagrams, and FEA stress heatmaps within 24 hours of inquiry.